 BRJ Medical
Engineered for tropical climate durability, stringent barrier performance, and rapid deployment in clinical and industrial facilities.
A Comprehensive Market Intelligence Report on Commercial Demand, Infection Control Protocols, and Supply Chain Integration in the Western Province Hub.
As the primary industrial port and economic engine of the Western Province in the Solomon Islands, Noro represents a vital nexus for tuna processing, maritime transport, regional health services, and municipal infrastructure. The demand for industrial-grade barrier packaging, steam sterilization autoclaves, and chemical indicators in Noro has escalated rapidly driven by strict export food safety protocols (HACCP) and modern healthcare mandates.
Factories operating within the Noro industrial zone require specialized sterilization media capable of enduring high tropical ambient humidity while maintaining 100% microbial barrier integrity over long storage cycles.
Sterilization supplies factories servicing the Pacific region face unique environmental stresses: salt-spray marine environments, persistent relative humidity exceeding 85%, and logistics lead times. High-performance medical packaging, such as medical-grade paper combined with PET/PP multi-layer laminated film, prevents moisture penetration and seal degradation.
Pioneering automated surgical device production and high-grade sterilization supply chains for international distribution.
Founded in May 2004, Jiangsu BRJ Medical Co., Ltd. is a leading manufacturer specializing in the research, development, production, and distribution of high-quality surgical sutures, surgical needles, and other related medical instruments.
We are committed to providing a wide range of products that meet the highest quality standards both domestically and internationally. Our products comply with major certifications including CE, ISO 13485, ISO 14001, ISO 45001, and we hold all the necessary production licenses to meet global market requirements. This ensures that every product we manufacture adheres to stringent safety, reliability, and effectiveness standards.
At Jiangsu BRJ Medical Co., Ltd., we firmly believe in the importance of innovation and continuous improvement. Our philosophy is built on modern techniques, superior quality, and complete customer satisfaction. Over the years, we have heavily invested in developing and integrating advanced technologies into our manufacturing processes. As a result, we have earned 29 invention patents and have successfully implemented fully automated production systems, which not only enhance product quality but also increase operational efficiency. This has helped us maintain our competitive edge in the ever-evolving healthcare industry.
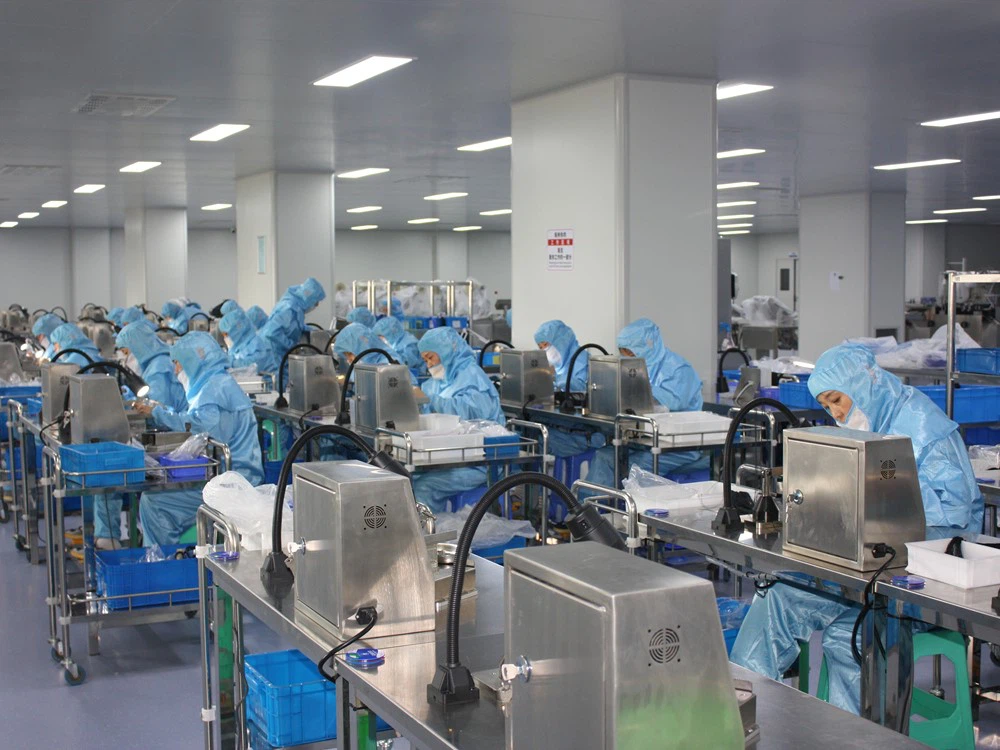
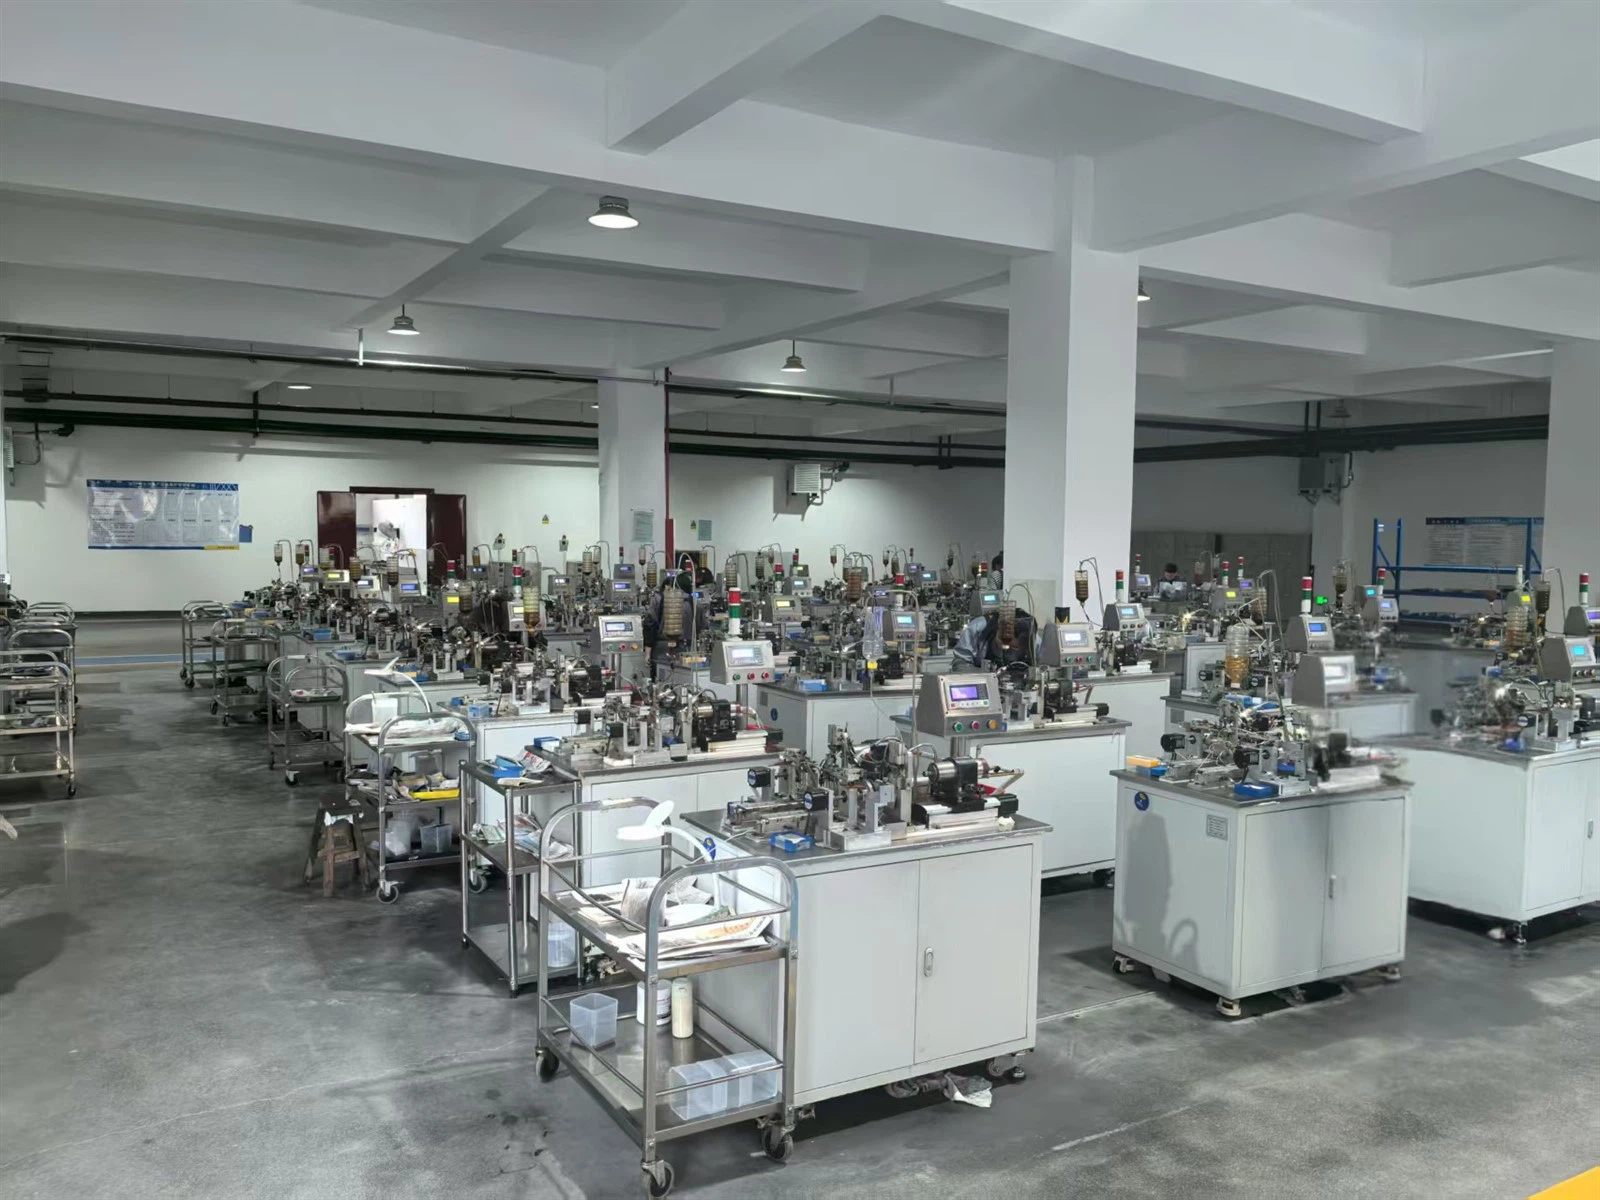
Our commitment to excellence has earned us recognition in numerous international markets. Our products are highly regarded for their superior performance, reliability, and precision in various medical applications. We have built strong and lasting relationships with healthcare institutions, hospitals, and distributors around the world, allowing us to contribute to improving patient outcomes and advancing medical practices globally.
Jiangsu BRJ Medical Co., Ltd. is driven by a passionate and dedicated team that works tirelessly to ensure that we meet the needs of the healthcare community. We value our business relationships with partners both at home and abroad and strive to make a meaningful impact on global healthcare. We welcome all interested parties to reach out and collaborate with us as we continue to improve and innovate in the field of medical technology.
Our Vision: To become a world-class leader in medical device manufacturing by consistently offering innovative, high-quality solutions that support healthcare professionals and improve patient care worldwide.
Architectural Innovations in Barrier Materials, Ethylene Oxide Chambers, and Automated Retort Systems.
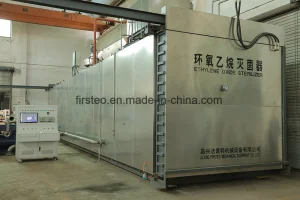
Utilizing high-density polyethylene (HDPE) combined with peelable composite films to prevent tearing during high-pressure steam and gas sterilization cycles.
Integrating non-toxic, lead-free water-based ink indicators that transition cleanly under EO Gas, Steam, and Formaldehyde exposure without risk of ink transfer.
Developing temperature-sensitive hydrogen peroxide plasma compatible packaging for surgical instrumentation delicate to heat stress.
Implementation of IoT-driven data logging across sterilization chambers to record pressure gradients, humidity, and temperature profiles in real-time.
Comprehensive solutions designed for hospital sterile processing departments (SPD) and industrial processing plants in Noro.


Leveraging Jiangsu's automated manufacturing hubs for seamless maritime shipment to Noro Port.
By automating suture attachment, pouch forming, and ultrasonic sealing, Jiangsu BRJ Medical minimizes human intervention, eliminating initial bio-burden and ensuring high dimensional uniformity across millions of units annually.
Direct factory-to-port sourcing allows commercial entities and medical distributors in Noro to access OEM grade sterilization wraps, indicator strips, and autoclaves at direct manufacturer pricing without intermediary markups.
All bulk export cartons destined for South Pacific ports are encased in moisture-proof heavy-duty corrugated cartons with desiccants, ensuring 100% dry arrival despite transshipment cycles across tropical equatorial seas.
Connecting medical device manufacturing with local healthcare, fisheries, and agro-processing demands.
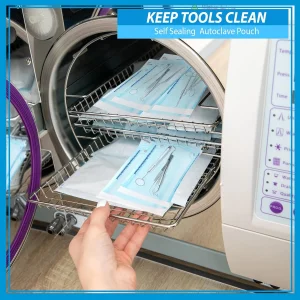
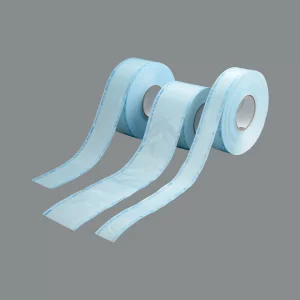
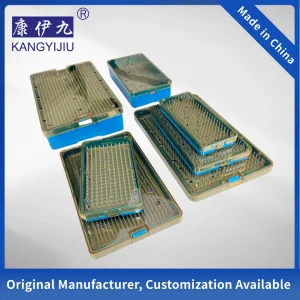
Providing self-sealing pouch reels, dental autoclaves, and PPSU disinfection trays to local clinics, ensuring sterile instrument storage and compliance with regional health authority infection prevention protocols.
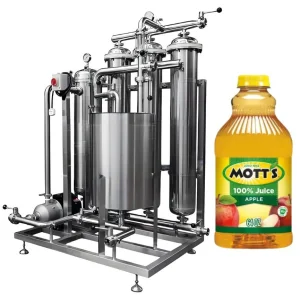
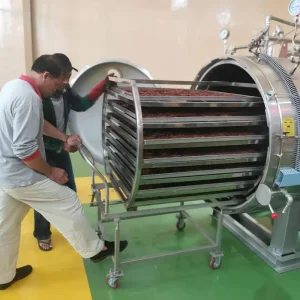
High-temperature retort autoclave machinery designed for food sterilization, juice clarification, and agricultural thermal processing, guaranteeing microbial shelf-stability for export products.
Commercial steam sterilizers for processing bio-hazardous waste generated by maritime vessels docking at Noro Port, preventing non-indigenous biological contamination of coastal ecosystems.
Our commitment to global standards guarantees that every product entering the Noro market is fully certified and tested.
Comprehensive Quality Management System specific to medical device design and manufacturing safety.
Full European Conformity certification allowing unhindered deployment in international medical channels.
Environmental Management certification ensuring clean manufacturing processes with minimal ecological impact.
Occupational Health & Safety management guaranteeing safe working environments for all production technicians.
Expert answers regarding technical specifications, customs compliance, and shipping logistics to Noro.
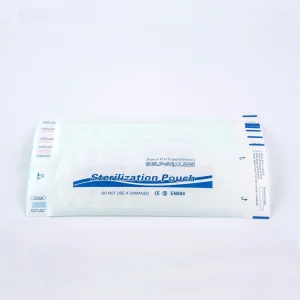
Our sterilization pouches utilize heavy-duty medical paper combined with multi-layer PET/PP film sealed with moisture-resistant medical grade adhesive. This guarantees micro-pore stability and long-term barrier retention even under humidity levels exceeding 85% RH.
Standard ocean freight lead time from major Chinese ports (Shanghai/Ningbo) to Noro Port is typically between 18 to 28 days depending on shipping line schedules. Express air shipping for urgent consumable supplies is available via Honiara hubs.
Yes, backed by 29 invention patents and automated production systems, we offer complete OEM/ODM customization for sterilization pouches, wraps, and indicator prints according to client specifications and regulatory demands.
Every shipment is accompanied by Certificates of Conformance (CoC), ISO 13485 quality control reports, CE compliance documentation, and batch sterilizing validation records guaranteeing full traceability.
Explore our full line of specialized sterilization autoclaves, food retorts, packaging, and water purification systems for Noro.
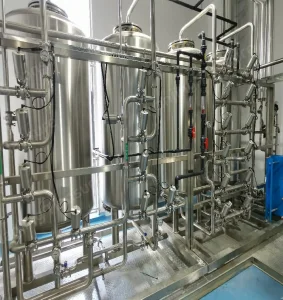
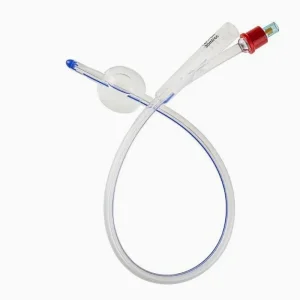
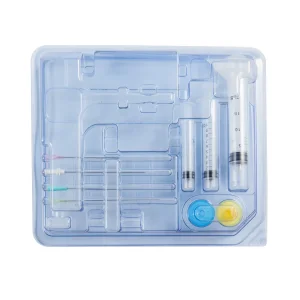
Get in touch with our technical engineering team for bulk wholesale quotes, custom OEM packaging requirements, and expedited shipping rates to Noro, Solomon Islands.
Send Inquiry Now