 BRJ Medical
Explore our top-tier catalog engineered for precision, reliability, and modern clinical performance.
Decades of dedicated engineering, establishing global trust in medical and personal care solutions.
Founded in May 2004, Jiangsu BRJ Medical Co., Ltd. is a leading manufacturer specializing in the research, development, production, and distribution of high-quality surgical sutures, surgical needles, and other related medical instruments.
We are committed to providing a wide range of products that meet the highest quality standards both domestically and internationally. Our products comply with major certifications including CE, ISO 13485, ISO 14001, ISO 45001, and we hold all the necessary production licenses to meet global market requirements. This ensures that every product we manufacture adheres to stringent safety, reliability, and effectiveness standards.
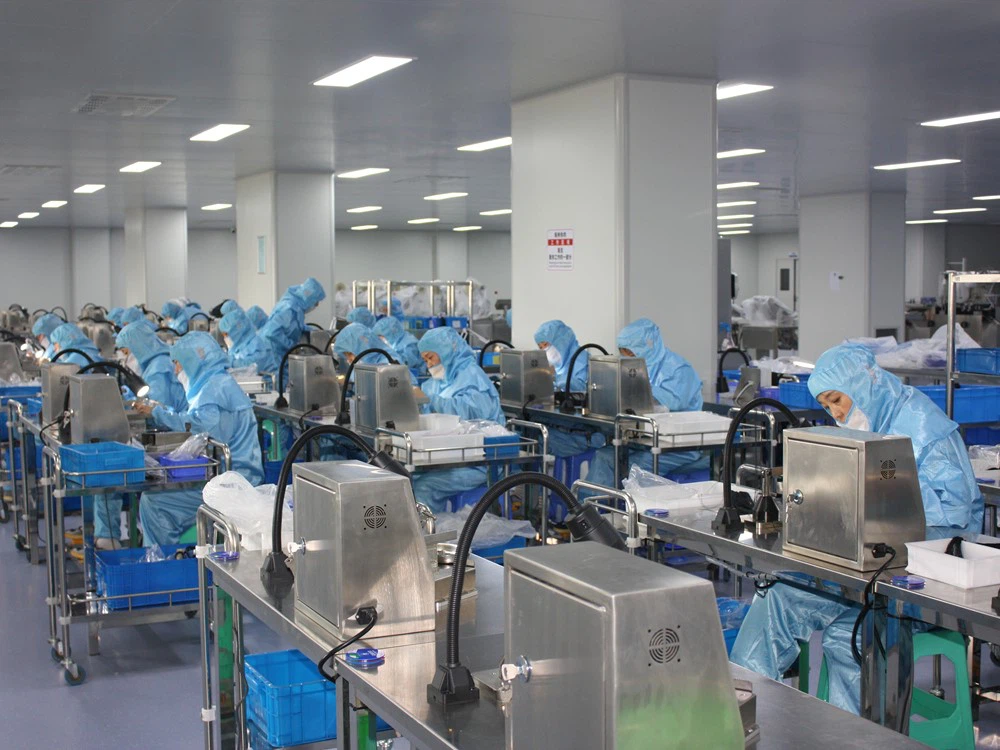
At Jiangsu BRJ Medical Co., Ltd., we firmly believe in the importance of innovation and continuous improvement. Our philosophy is built on modern techniques, superior quality, and complete customer satisfaction. Over the years, we have heavily invested in developing and integrating advanced technologies into our manufacturing processes. As a result, we have earned 29 invention patents and have successfully implemented fully automated production systems, which not only enhance product quality but also increase operational efficiency. This has helped us maintain our competitive edge in the ever-evolving healthcare industry.
Our commitment to excellence has earned us recognition in numerous international markets. Our products are highly regarded for their superior performance, reliability, and precision in various medical applications. We have built strong and lasting relationships with healthcare institutions, hospitals, and distributors around the world, allowing us to contribute to improving patient outcomes and advancing medical practices globally.
Jiangsu BRJ Medical Co., Ltd. is driven by a passionate and dedicated team that works tirelessly to ensure that we meet the needs of the healthcare community. We value our business relationships with partners both at home and abroad and strive to make a meaningful impact on global healthcare. We welcome all interested parties to reach out and collaborate with us as we continue to improve and innovate in the field of medical technology.
Our Core Values:
Continuous Innovation: Our ongoing efforts to stay ahead of technological trends and incorporate the latest advancements in our production processes.
Commitment to Quality: Each of our products undergoes rigorous quality control and testing to ensure that we deliver only the best to our customers.
Global Responsibility: We aim to contribute positively to public health, environmental sustainability, and social well-being through our products and practices.
Our Vision: To become a world-class leader in medical device manufacturing by consistently offering innovative, high-quality solutions that support healthcare professionals and improve patient care worldwide.
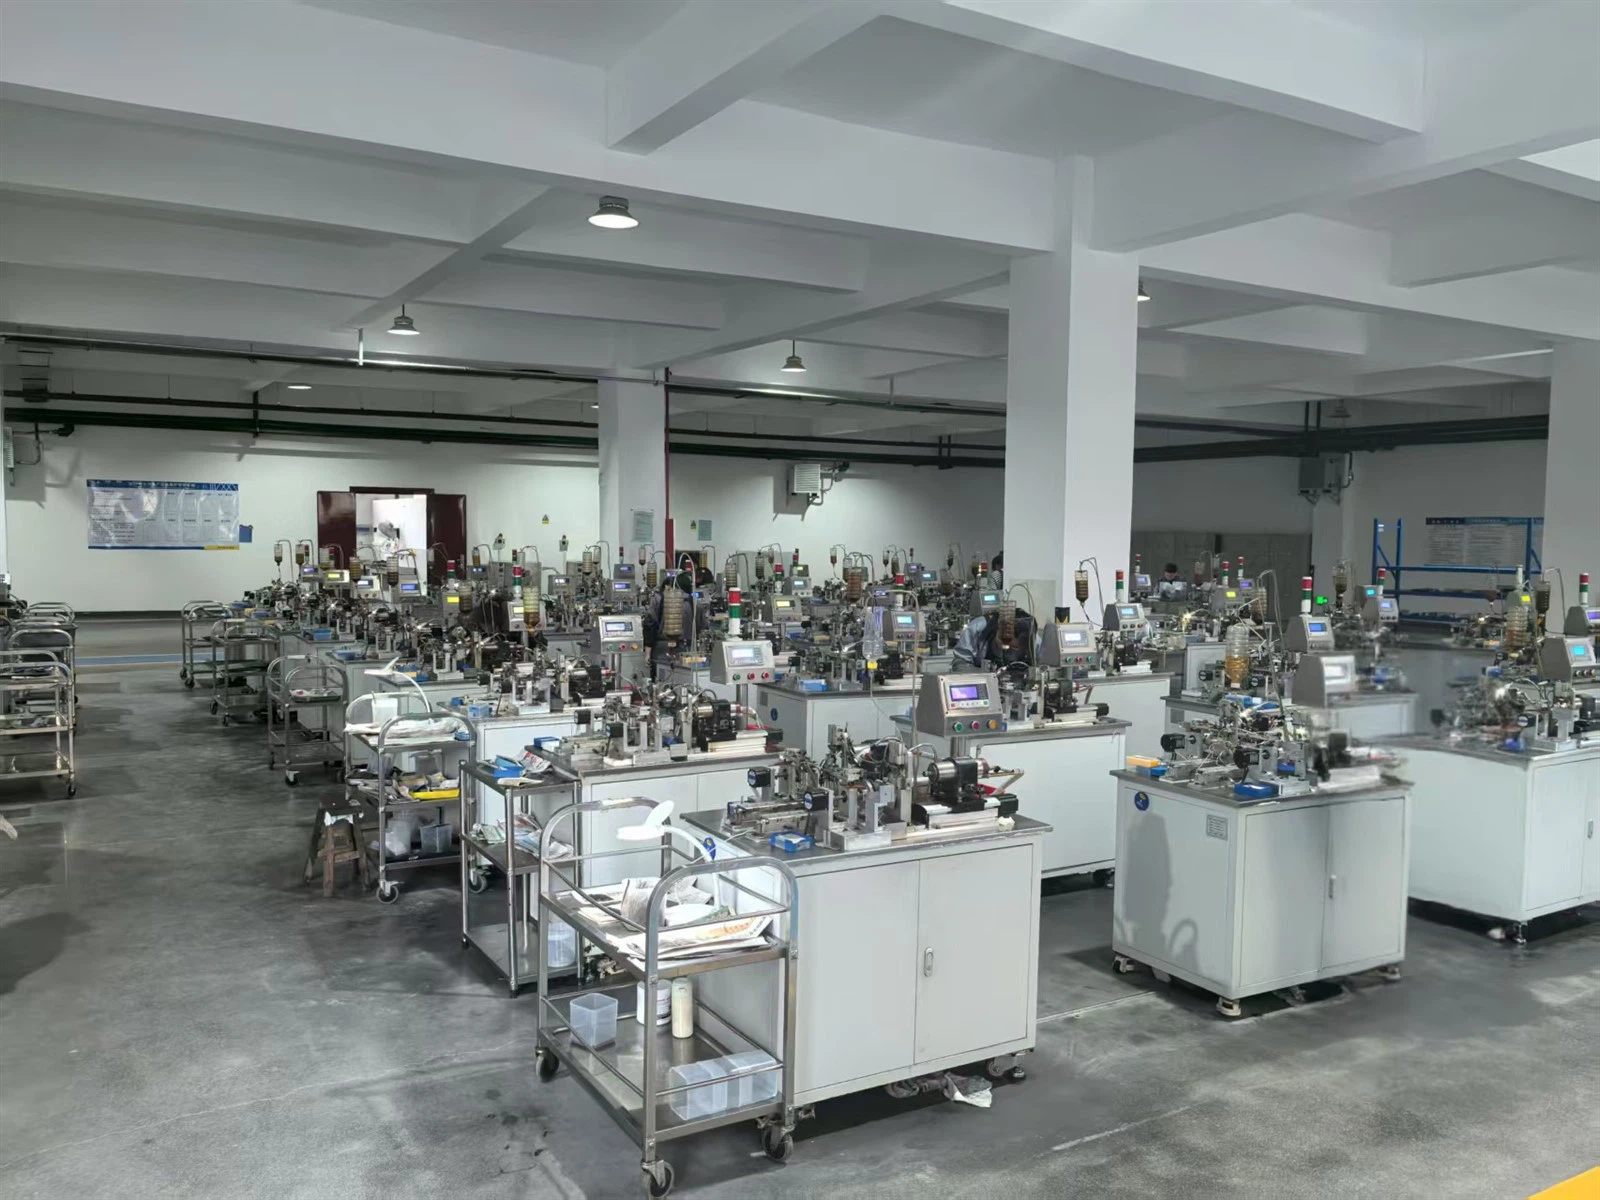
Navigating the shifting demands of modern international procurement and health safety standards.
International procurement managers demand resilient supply chains. As a premier China exporter, we bridge manufacturing efficiency with strict international compliance, ensuring zero-latency supply fulfillment for global institutional partners.
Leveraging fully automated production environments minimizes human error and maximizes unit consistency. Our 29+ patented technologies guarantee top-grade output across personal care formulations and medical devices.
With CE, ISO 13485, ISO 14001, and ISO 45001 credentials, our manufacturing framework preemptively meets the stringent import regulations of the EU, North America, and emerging global healthcare markets.
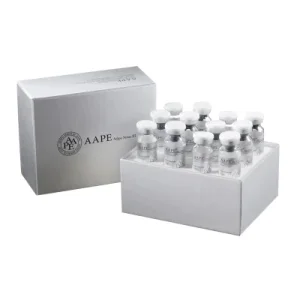
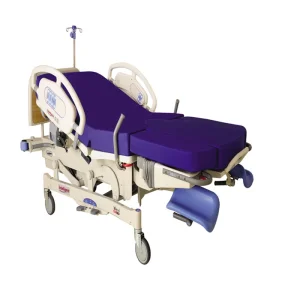
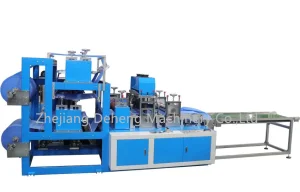
Comprehensive solutions ranging from surgical instruments to high-efficiency industrial mixers.



Pioneering the next generation of smart manufacturing in personal care and medical distribution.
Complete integration of IoT sensors across assembly lines to monitor particulate levels, sterilization temperatures, and packaging integrity in real-time.
Adopting eco-friendly biodegradable materials for personal care packaging and reducing carbon emissions across our ISO 14001 certified facilities.
Deploying AI-driven predictive logistics for international B2B buyers to optimize inventory turnover and reduce transit bottlenecks worldwide.
Expert insights for global B2B procurement partners seeking reliable manufacturing collaboration.
Our manufacturing operations strictly comply with global standards, holding CE, ISO 13485 (medical devices quality management), ISO 14001 (environmental management), and ISO 45001 (occupational health and safety) certifications.
Yes. With our robust R&D infrastructure, 29+ invention patents, and automated production lines, we offer comprehensive OEM and ODM support tailored to international brand specifications.
Thanks to our fully automated production systems and scalable manufacturing capacity, standard bulk export orders are efficiently processed and shipped within optimized delivery windows.
Every single batch undergoes rigorous multi-tier testing—from raw material inspection to sterile packaging verification—ensuring 100% compliance with international export safety benchmarks.